

AI & Machine Learning
Computer Vision for Quality Control: Costs and Returns in Manufacturing
Published:
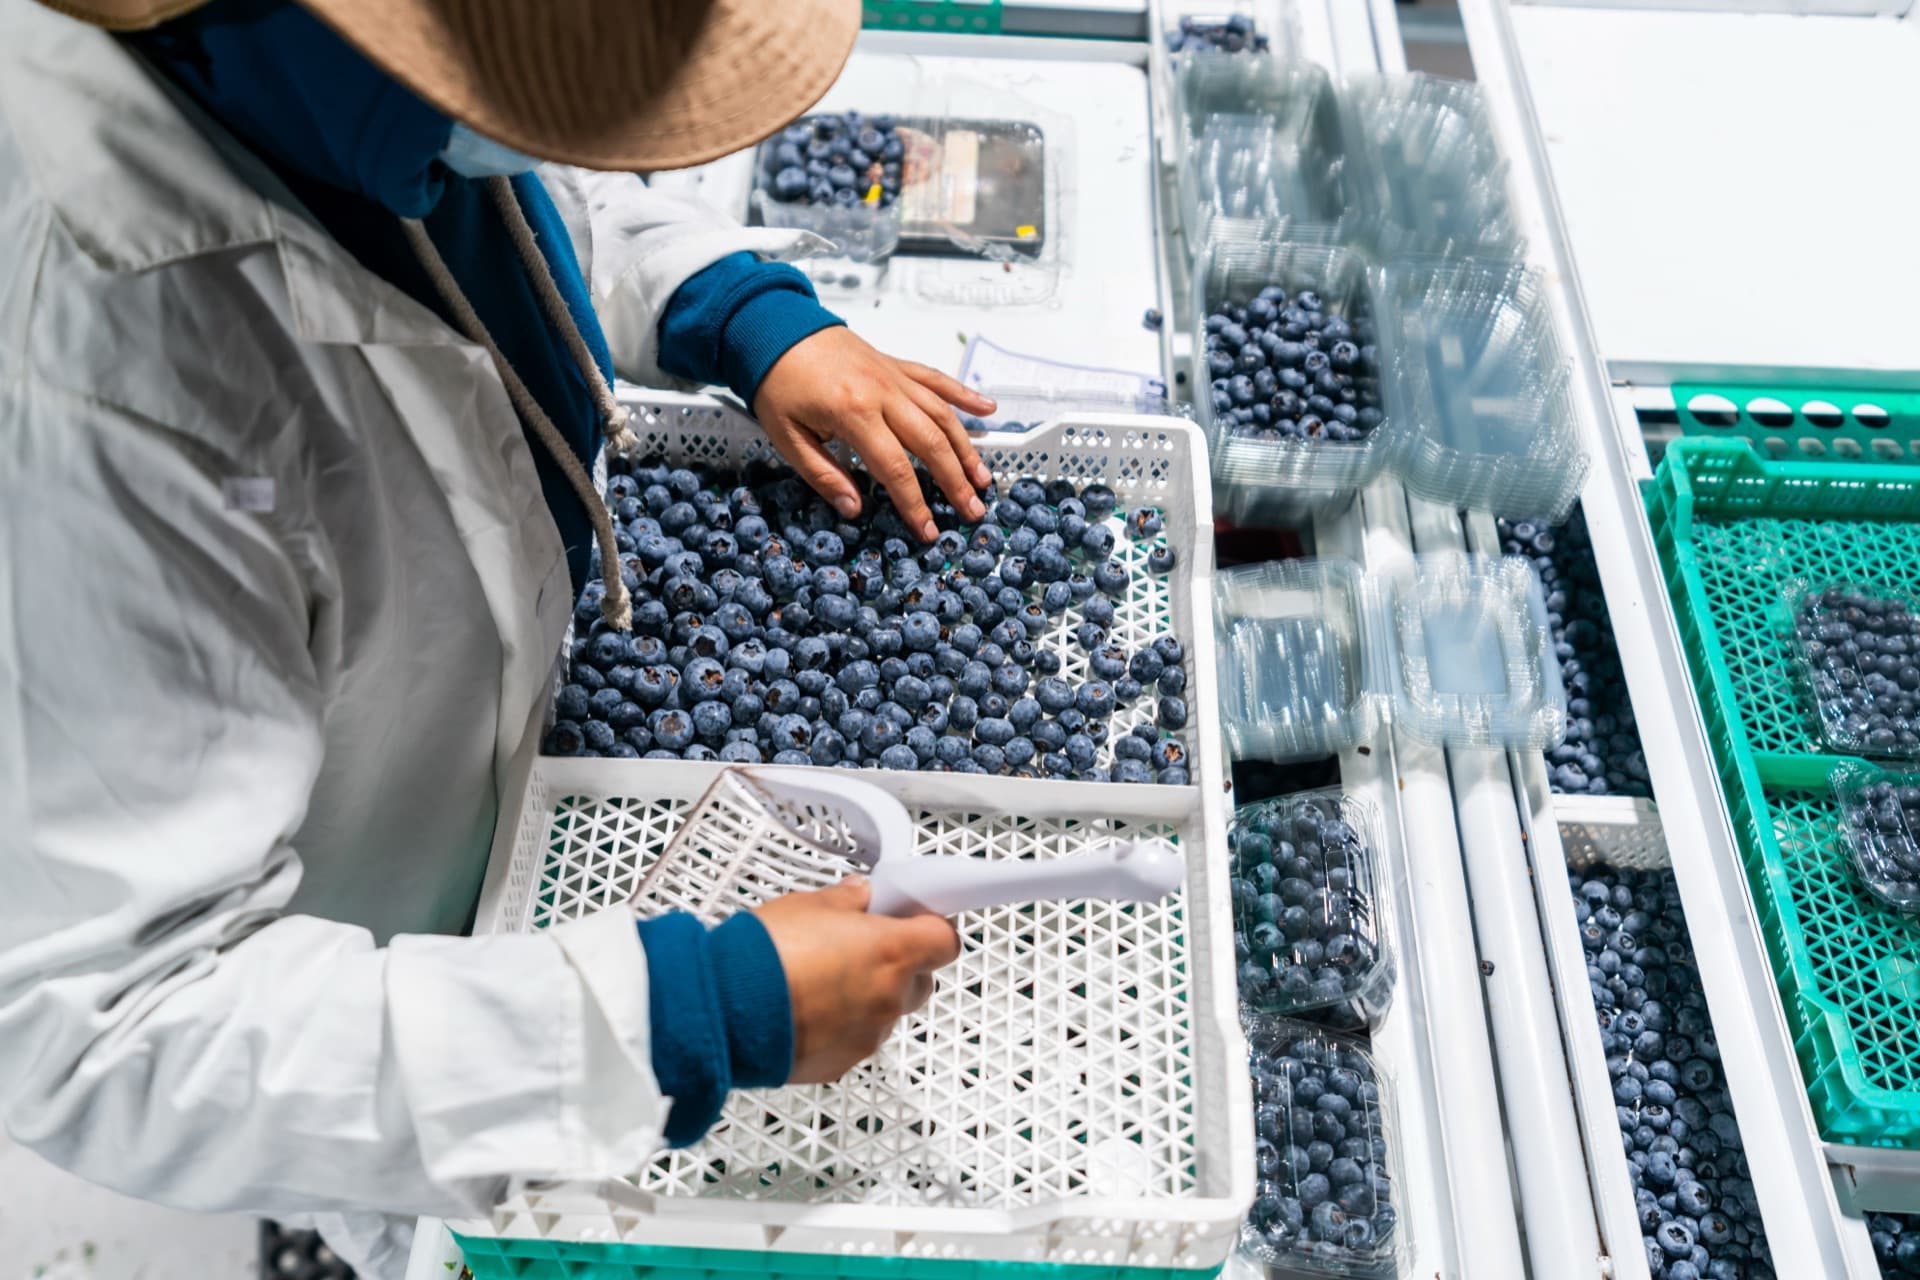
Key Takeaways: Computer vision achieves 90-99% defect detection and operates up to 80% faster than manual inspection. For manufacturers with high volumes, the investment pays for itself within 6 to 12 months. This article provides a complete cost-benefit analysis, discusses technical requirements, and shows how Dutch subsidies lower the implementation threshold.
Computer vision detects production defects with 90-99% accuracy and runs 24/7 without fatigue, making it the most cost-effective quality investment of this decade for high-volume manufacturers
Manual quality control is one of the last bastions of human inspection in the automated factory. That is not because technology was lacking, but because the required accuracy and reliability were until recently not achievable. That situation has fundamentally changed. Modern computer vision systems, powered by deep learning, achieve detection rates that surpass human inspectors at a fraction of the ongoing costs.
The Dutch manufacturing sector counts approximately 68,000 companies and generates 12% of GDP. Despite this scale, only 14% of manufacturers use AI-driven quality control, according to FME research from 2025. The reason is not scepticism about the technology, but uncertainty about costs, implementation complexity, and ROI. This article removes that uncertainty with concrete figures and practical examples.
What computer vision can do in quality control
Computer vision for quality control works by combining cameras with AI models trained to recognise deviations. The system compares each produced part against a learned reference image and classifies it as approved, rejected, or borderline. Applications range from surface inspection (scratches, dents, colour deviations) to dimensional control (measurements, component positioning) and assembly verification (are all parts present and correctly placed).
The technology is not new, but performance has improved exponentially over the past three years. Where earlier systems worked with rigid rules ("if pixel X differs from reference, reject"), modern systems use convolutional neural networks that learn from thousands of examples of good and defective products. The result: 90-99% detection accuracy depending on defect type and production environment, compared to 70-85% for experienced human inspectors who show significant performance degradation after 30 minutes of concentration on average.
Speed is equally impressive. A typical computer vision system inspects 60 to 300 parts per minute, depending on product size and inspection complexity. Manual inspection achieves 5 to 20 parts per minute. That factor-10-to-15 difference is not only a speed gain but also a capacity increase that enables growth without proportional workforce expansion.
What does a computer vision system cost?
The costs of a computer vision system for quality control consist of hardware, software, integration, and ongoing maintenance. The total initial investment ranges from 25,000 euros for a simple single-camera setup to 250,000 euros for a multi-camera system with full line integration.
Hardware includes industrial cameras (2,000-15,000 euros per unit depending on resolution and speed), lighting (1,000-8,000 euros per inspection station, crucial for consistent image quality), a processing unit with GPU (3,000-15,000 euros), and mounting structures. For a typical single-station setup, hardware costs amount to 8,000 to 35,000 euros.
Software and model development form the largest portion of the investment. Training a custom computer vision model requires collecting and labelling thousands of product images, training the model, validation, and fine-tuning. This phase costs 15,000 to 80,000 euros depending on the number of defect types, variation in product appearance, and required accuracy. When producing five different product lines with ten possible defect types each, the training effort is significantly greater than for a single product line with three defect types.
Integration with existing production lines and MES/ERP systems costs 5,000 to 40,000 euros. This includes physically fitting cameras into the production line, connecting to PLC controls for automatic rejection, and integrating inspection results into quality management systems. For existing, older production lines, the integration effort is typically greater than for newly designed lines.
Ongoing costs amount to 8,000 to 25,000 euros per year for maintenance, software updates, model retraining (for new product variants or defect types), and calibration. Cloud costs for model inference are minimal with local processing (the model runs on the processing unit in the factory) but can amount to 200 to 800 euros per month if you opt for cloud-based processing.
The ROI calculation: when does it pay for itself?
The payback period for computer vision quality control depends on three factors: the current volume of manual inspection, the failure rate, and the cost of undetected defects. Let us walk through a realistic example.
Consider a manufacturing company producing 500,000 parts per year with a current defect rate of 2%. Manual inspection costs two full-time inspectors (together 90,000 euros per year) and detects 80% of defects. The remaining 20% undetected defects (2,000 parts) lead to customer complaints, returns, and reputational damage, estimated at 15 euros per undetected defect, totalling 30,000 euros per year in failure costs.
A computer vision system costing 75,000 euros (hardware, software, integration) with annual costs of 15,000 euros detects 95% of defects. The two inspectors are redeployed to higher-value tasks (or one is not replaced upon departure, saving 45,000 euros). Failure costs drop from 30,000 to 7,500 euros per year.
The annual saving: 45,000 euros (personnel) + 22,500 euros (failure costs) = 67,500 euros. Minus the annual operational costs of 15,000 euros, a net annual saving of 52,500 euros remains. The payback period: 75,000 / 52,500 = 17 months. At higher volumes or higher failure costs, the payback period drops to 6 to 12 months.
Technical requirements and pitfalls
A successful computer vision implementation requires more than good hardware and software. Lighting is decisive: inconsistent lighting is the primary cause of false positives and missed defects. Invest in controlled lighting that is independent of ambient light, seasonal variations, and lamp wear.
Training data is the second critical factor. The model must be trained on sufficient examples of both approved and defective products. A rule of thumb is at least 500 labelled images per defect type, although modern techniques such as data augmentation and transfer learning can reduce the required quantity. Labelling training data is labour-intensive: expect 2-5 minutes per image for complex defects, which at 5,000 images quickly amounts to 200-400 hours.
A common mistake is underestimating the variation in product appearance. A product that looks uniform under laboratory conditions shows variation in practice due to material differences, production tolerances, and environmental conditions. The model must be robust enough to distinguish this normal variation from actual defects. This requires a representative training set covering the full range of normal product variation.
Sector-specific applications
In the metals industry, computer vision detects weld defects, surface imperfections, and dimensional deviations. For weld inspection, modern systems achieve detection rates of 97% for porosity, cracks, and incomplete fusion, compared to 85% for certified weld inspectors. The investment is particularly profitable for companies working under NEN or ISO quality standards where 100% inspection is required.
In the plastics industry, computer vision identifies colour deviations, surface defects, and shape deviations in injection-moulded products. The challenge here is the high production speed: injection moulding machines produce a part every 15 to 60 seconds, requiring real-time inspection with minimal latency. Modern edge computing solutions enable inspection times of under 100 milliseconds per part.
In the food industry, computer vision is deployed for detecting foreign objects, checking labelling, and assessing product quality (ripeness, colour, size). Strict HACCP and BRC standards make automated inspection particularly valuable, and ROI is typically 30-50% higher than in other sectors due to the high costs of product recalls.
Subsidies and financing options
Computer vision projects qualify for multiple Dutch subsidies. The WBSO compensates up to 32% of labour costs for the development of the vision model and integration software. On a project with 40,000 euros in software development costs, you save up to 12,800 euros.
The MIT scheme offers subsidies for R&D collaboration projects. If you collaborate with a knowledge institution or another SME on an innovative vision system, up to 35% of project costs can be subsidised.
Additionally, there are sector-specific schemes through industry associations and regional development agencies. The SMITZH programme in South Holland and the Smart Industry Fieldlabs offer co-financing and access to test facilities. Enquire with your regional manufacturing network about current opportunities.
Edge AI versus cloud: where does your model run?
An important architectural choice is whether the vision model runs locally on the factory floor (edge computing) or in the cloud. Both options have clear advantages and disadvantages that directly affect costs, latency, and privacy.
Edge computing means the GPU processing unit sits physically next to the production line. The advantage is minimal latency (under 50 milliseconds), complete independence from internet connectivity, and maximum data privacy. Image data never leaves the factory, which is relevant for companies with sensitive production processes or strict IP protection. The disadvantages are higher initial hardware costs (8,000-15,000 euros per processing unit) and the need to update firmware and models locally.
Cloud-based processing offers more flexibility in computing power and makes it easier to manage and update models centrally. Latency is higher (200-500 milliseconds depending on connection quality) and there are ongoing costs of 200 to 800 euros per month for compute and data transfer. For applications where real-time feedback is not critical, for example end-of-line inspection before shipping, cloud is a cost-effective alternative.
In practice, 72% of manufacturing companies choose edge computing for inline inspection (directly in the production line) and cloud computing for offline inspection (sampling after production). A hybrid approach where the model runs locally but training data and model updates are distributed via the cloud combines the best of both worlds.
Implementation roadmap for SMEs
A successful implementation follows a phased approach. In months one and two, you conduct a feasibility analysis: which defects do you want to detect, what is the current volume and failure rate, and what are the technical requirements (lighting, speed, product variation)? Cost: 3,000-8,000 euros.
In months three to five, the proof of concept follows: a camera setup on a limited section of the production line, trained on the most common defect types. Goal: validation that the required detection accuracy is achievable. Cost: 15,000-35,000 euros.
In months six to nine, you scale to a full implementation: integration with the production line, connection to quality management systems, and operator training. Cost: 20,000-80,000 euros depending on scale.
After implementation, a continuous optimisation phase follows: model improvement based on production data, expansion to new defect types and product variants, and periodic recalibration. Budget: 8,000-25,000 euros per year.
Common mistakes and how to avoid them
The first pitfall is scaling too quickly after a successful proof of concept. A model that works on a controlled test setup does not automatically perform equally well on a full production line with variation in lighting, product flow, and ambient temperature. Always plan a validation phase on the actual production line, with sufficient data from realistic conditions.
The second mistake is neglecting operator acceptance. A system that detects defects but whose alerts are ignored or distrusted by operators delivers no value. Invest in training, explain how the system works, and involve operators in the validation process. Deloitte research shows that change management determines 25-35% of the success in industrial AI implementations.
The third pitfall is underestimating ongoing model maintenance. Product variants change, new materials are introduced, and seasonal influences affect image quality. Without periodic retraining, every vision model degrades. Plan at least two retraining cycles per year, or implement continuous monitoring that automatically signals when model performance drops below the threshold.
Conclusion: the threshold is lower than you think
Computer vision for quality control is no longer a futuristic technology but an investment that pays for itself. The combination of declining hardware costs, mature software, and available subsidies makes the threshold achievable even for SME manufacturers. Start with a feasibility analysis on your most critical inspection process, validate the technology in a proof of concept, and scale once the results are in.
Want a concrete picture of what computer vision could mean for your production line? Get in touch for a no-obligation conversation where we map your inspection process and provide an initial feasibility estimate.
Get the AI-subsidy radar
1 email per month. New subsidies, deadlines, and what changed for SMEs. 5-minute read.
Unsubscribe with one click. No spam, ever.
Keep reading
Related articles
AI & Machine Learning
Computer Vision for Quality Control: Implementation and Cost for Manufacturing
How manufacturers deploy computer vision for automated quality control, from data requirements and camera setup to line integration, false positives, and the cost of a production-grade implementation.
Read more →
AI & Machine Learning
AI subsidies for manufacturing: how Dutch manufacturers fund predictive maintenance, quality control and process optimisation in 2026
Dutch manufacturing leads in AI adoption. Discover which subsidies fund predictive maintenance, quality control and process optimisation for your factory.
Read more →
AI & Machine Learning
AI in Construction: Project Planning, Cost Estimation, and Safety
How AI helps construction companies with more accurate planning, cost estimates, and safety monitoring. Five applications with the numbers behind them.
Read more →

Let's talk business
Do you want to know how we can help you grow your business? Schedule free consultation with one of our experts and discover the possibilities.



