AI & Machine Learning
Computer Vision for Quality Control: Implementation and Cost for Manufacturing
Published:
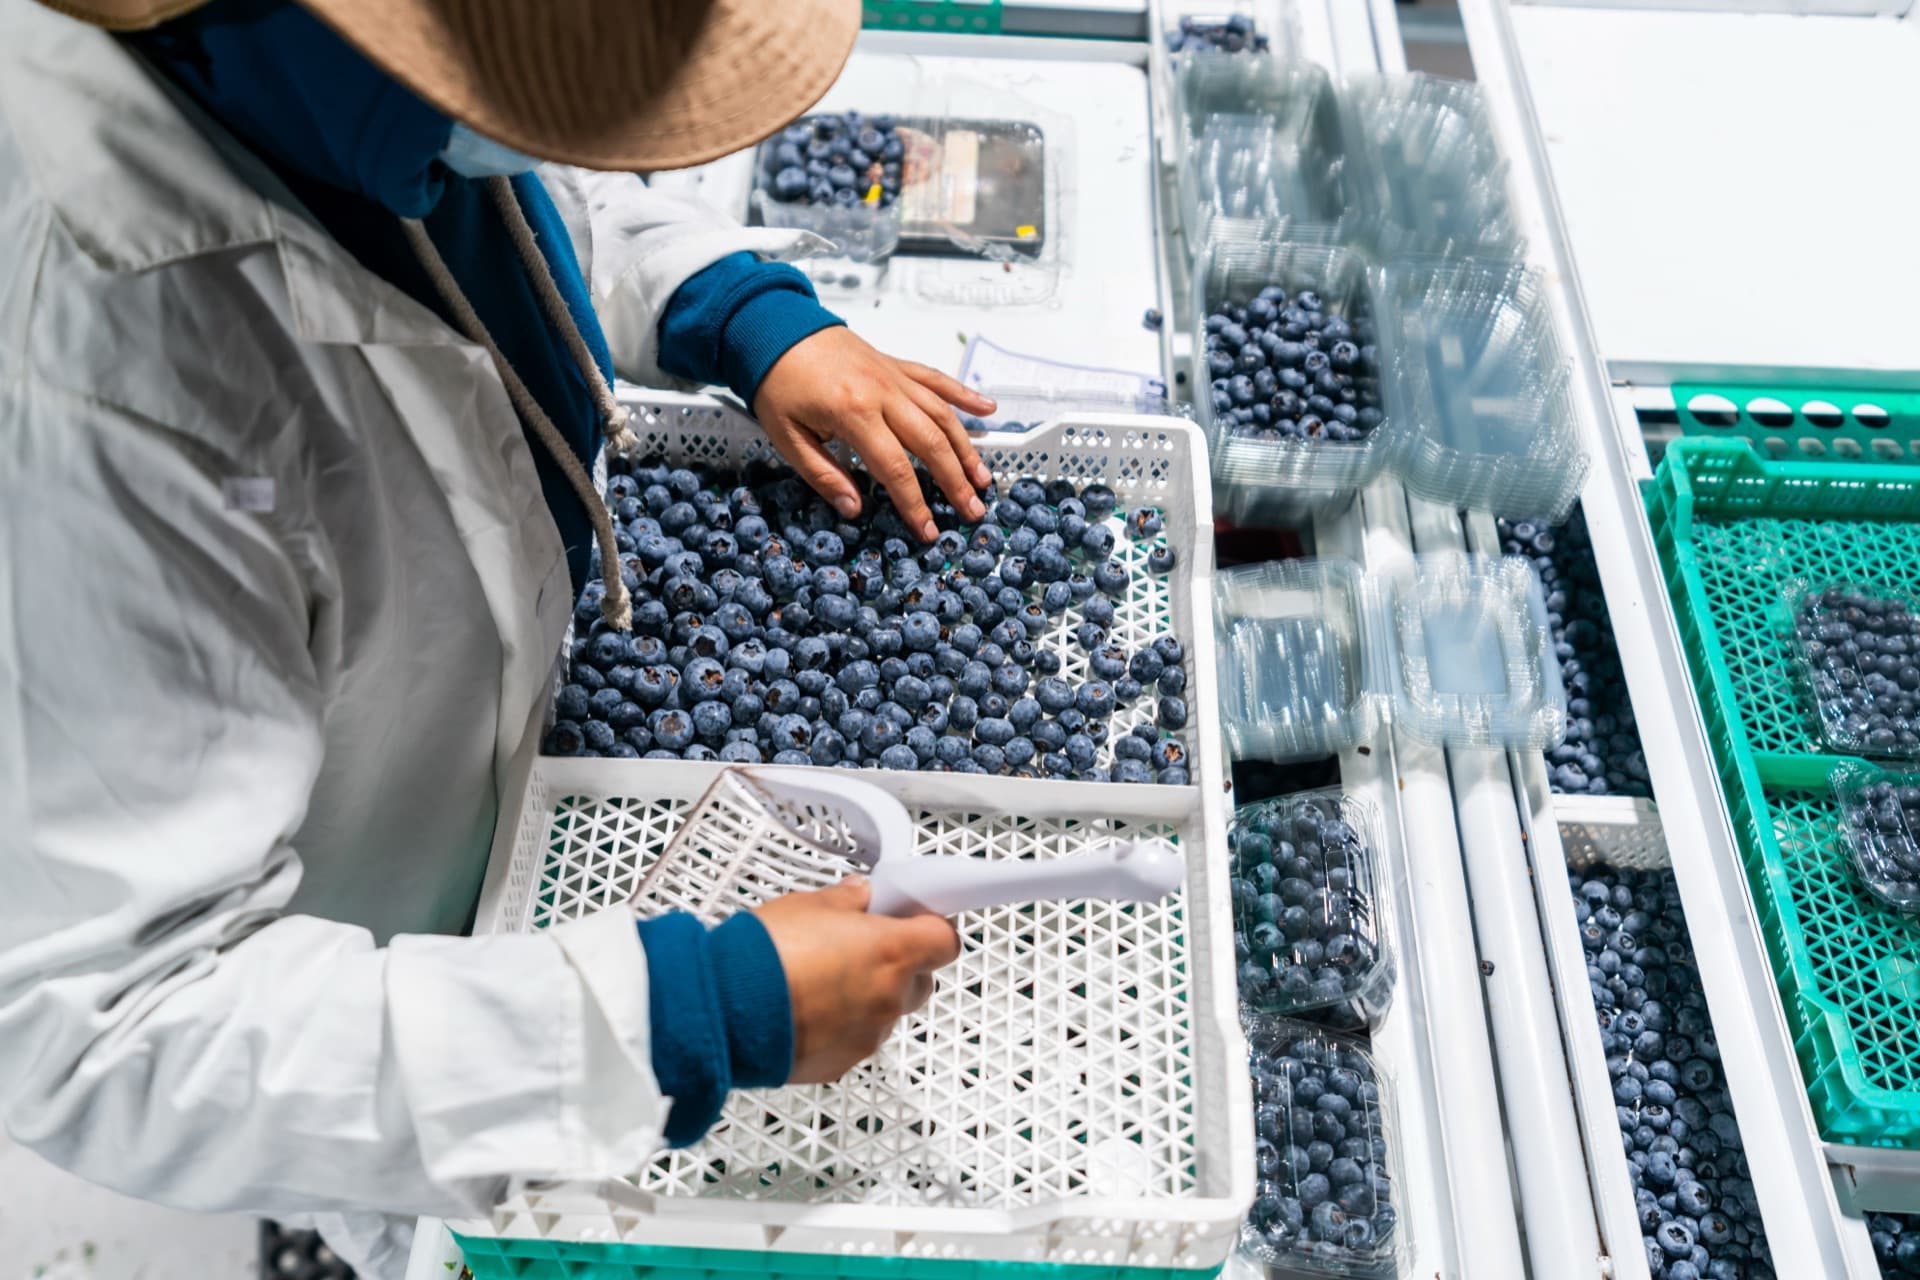
Key points: Computer vision shifts quality control from sample-based, manual inspection to continuous, automated control across the full product stream. Detection rates of 99%+ are achievable, but success depends less on the model than on image quality, representative training data and line integration. This article covers implementation end to end, data requirements, camera setup, false positives, line integration and the cost of a production-grade solution.
Why manual inspection falls short at scale
Manual quality inspection has two structural limitations. It is sample-based, an inspector reviews a fraction of production, and it is inconsistent, because fatigue and differences in interpretation play a role. At high volumes this means defects slip through and quality varies with who is on shift.
Computer vision addresses both: it inspects every product instead of a sample, and it does so consistently, against the same criteria, 24 hours a day. That shifts quality control from an after-the-fact sample to real-time control across the full stream. For manufacturers where a slipped-through defect leads to recalls, warranty claims or reputational damage, that is a fundamentally different risk profile.
Data requirements: the decisive factor
Most of the work sits not in the model but in the images. A computer vision model learns to recognise defects from examples, so you need representative, labelled images of both good products and the defect types you want to detect.
How many images? For clear, consistent defects a few hundred labelled examples per class can suffice. For rare or subtle defects more are needed, and rare defects are exactly the hard ones, because by definition you have few examples of them. Techniques like data augmentation (synthetically generating variants) and transfer learning (building on a pre-trained model) lower that barrier, but do not replace representative data.
The practical consequence: a serious project starts with a phase in which images are collected and labelled under controlled conditions. A partner that skips this and quotes a fixed price immediately usually underestimates where the complexity sits.
Camera setup and lighting
An underrated point is that image quality is largely determined by the physical setup: cameras, lenses and especially lighting. Controlled, consistent lighting makes the difference between a model that works reliably and one that stumbles over shadows and reflections. In practice, optimising the setup is often as important as training the model.
False positives versus missed defects
No system is perfect, and the heart of a good implementation is the trade-off between two kinds of error: missing a defect (false negative) and rejecting a good product (false positive). That trade-off is not a technical but a business decision: what does a slipped-through defect cost versus a wrongly rejected product?
In a safety-critical application you tune the system strictly, better to reject a good product than to let a defect pass. In a cost-driven application you seek the balance that minimises total error cost. A mature implementation makes this trade-off explicit and adjustable, rather than aiming at an abstract "accuracy".
Line integration
The model only becomes valuable when it acts on the process. In practice it runs on edge hardware at the line, for low latency, so the decision is made before the product moves on, connected to the cameras. The output drives a physical action: reject, sorting into a separate stream, or an alert for an operator. And every decision is logged, so quality is traceable.
That connection to PLCs, sorting mechanisms and existing systems determines success as much as the model. It is precisely the phase where a project stalls between pilot and production: the model recognises defects in a test, but integration with the line is not arranged.
What it costs
Costs consist of three parts: hardware (cameras, lighting, edge compute), model development, and line integration. A scoped proof-of-concept on one defect type and one line is in the order of several thousand to tens of thousands of euros and validates whether the image quality and detection are feasible. A production-grade rollout across multiple lines and defect types runs higher. The biggest variable is invariably the availability of representative training images. An overview of what these applications deliver on average is in our machine learning ROI benchmark.
The pragmatic route
Start small and prove feasibility first: one line, one or a few defect types, a controlled setup. Agree upfront which detection rate and which balance between false positives and missed defects the system must reach to proceed. Only when that threshold is met do you scale up to more lines and defect types. That way you pay for certainty before you pay for scale.
Want to explore whether computer vision is feasible for your quality control? Get in touch, we assess your defect types, your image material and the feasibility of an implementation.
Frequently asked questions
How accurate is computer vision for quality control?
Well-trained systems reach detection rates of 99%+ on defined defect types, and inspect the full product stream in real time instead of a sample. The actual accuracy depends on image quality, defect variation and the amount of representative training images. The trade-off between missed defects and false positives is tuned to the cost of each type of error.
How many images are needed to train a computer vision model?
That depends on the complexity and variation of the defects. For clear, consistent defects a few hundred labelled examples per class can suffice; for rare or subtle defects more are needed, and techniques like data augmentation and transfer learning help. Collecting and labelling representative images is usually the largest part of the work.
What does a computer vision quality control system cost?
Costs consist of hardware (cameras, lighting, edge compute), model development and line integration. A scoped proof-of-concept on one defect type is in the order of several thousand to tens of thousands of euros; a production-grade implementation with line integration and operation runs higher, depending on the number of lines and defect types. The biggest variable is the availability of good training images.
How do you integrate computer vision with the existing production line?
The model typically runs on edge hardware at the line for low latency, connected to cameras with controlled lighting. The output drives an action, reject, sorting or an alert, and is logged for traceability. Integration with PLCs and existing systems is just as decisive for success as the model itself.
Get the AI-subsidy radar
1 email per month. New subsidies, deadlines, and what changed for SMEs. 5-minute read.
Unsubscribe with one click. No spam, ever.
Keep reading
Related articles
AI & Machine Learning
Computer Vision for Quality Control: Costs and Returns in Manufacturing
Discover how computer vision transforms defect detection in manufacturing, what implementation costs, and when the investment pays for itself.
Read more →
AI & Machine Learning
Machine Learning ROI Benchmark: What It Delivers by Use Case
An outcome benchmark for machine learning in practice, what the most common use cases measurably deliver, based on anonymised results from our projects combined with published industry ranges.
Read more →
AI & Machine Learning
What We Build: Machine Learning Projects and Their Impact
An anonymised overview of machine learning projects we put into production, for each project the technique and the impact in numbers, from forecast correction with seven-figure savings to recommendation engines and document intelligence.
Read more →

Let's talk business
Do you want to know how we can help you grow your business? Schedule free consultation with one of our experts and discover the possibilities.